
Downhole Tool Services
Hardfacing, Machining & Downhole Tool Repair in Houston, TX
Your stabilizers, reamers and mills wear out downhole. WeldIT rebuilds, hardfaces, machines and grinds them back to gauge all under one roof in our fabrication facility. We ensure inspection records and compliance on every tool.
One Houston Shop for the Full Life of a Downhole Tool
Drilling tools fail in predictable places: blades lose gauge, wear pads wash out, threads gall, bores score. Sending a tool to one vendor for welding, another for machining and a third for grinding adds weeks and leaves nobody accountable for the finished dimension.
WeldIT handles the whole job under one roof in northwest Houston. We strip and inspect the tool, rebuild worn areas, apply the right hardfacing for the formation, machine and grind to drawing, and ship it with a full inspection report. New-build components follow the same route from bar stock.
We work for drilling tool manufacturers, oilfield service companies, rental tool fleets and directional drilling companies across the Gulf Coast and Permian.
Our Expertise
Six Downhole Tool Services Under One Roof
From a worn stabilizer to a finished, gauged and documented tool, every step happens in our Houston shop.
Crushed carbide, insert, tile and spray-and-fuse systems matched to your formation, applied under controlled preheat.
Turning, milling and mill-turn for new components and re-machining repaired tools back to drawing.
TIG, MIG and flux core build-up that restores worn blades, journals, seal areas and bores.
CNC and manual grinding of hardfaced blades and cylindrical surfaces from 6 to 24 in. diameter.
Internal keyways, splines and blind features burned into hardened and hardfaced parts without distortion.
Dimensional checks, MT, PT and UT, with a full data package tied to the tool serial number.
Service 01
Tungsten Carbide Hardfacing for Downhole Tools
Hardfacing is a wear-resistant layer applied to the surfaces that contact the formation or the casing. Done right, it multiplies the footage a tool runs before it is pulled. Done wrong, the carbide washes out or the base metal cracks. We match the hardfacing system to your formation, tool design and budget, and we control preheat and cooling on every tool.
Choosing the Right Hardfacing
| System | How it is built | Best suited to | Relative cost |
|---|---|---|---|
| Crushed carbide composite | Crushed tungsten carbide particles, 1/8″ to 1/4″, in a tough nickel-based matrix, applied by torch | Soft to medium formations; milling and scraping tools with cutting-grade carbide | Lowest |
| Carbide insert with composite infill | Shaped tungsten carbide inserts set on the blade, gaps filled with fine composite | Medium formations; longer gauge life than composite alone | Mid |
| Carbide tile, brick pattern | Tungsten carbide tiles laid tight in a brickwork pattern with infill | Medium to hard, abrasive formations | Higher |
| Carbide tile, herringbone pattern | Tiles in a herringbone layout for maximum coverage and minimum exposed matrix | Hard, abrasive formations and high-flow areas where matrix washout is the failure mode | Highest |
| Cobalt-based alloy overlay | Weld-deposited cobalt alloy | Sealing faces, valve trim and sliding surfaces needing galling and corrosion resistance | Varies by area |
| Spray and fuse | Nickel-based powder with tungsten carbide, sprayed then fused | Thin, smooth wear layers on sleeves, shafts and plungers | Varies by area |
What You Get
- ✓Hardfacing on new tools and strip-and-redress of worn tools
- ✓Preheat, interpass and slow-cool control suited to 4140, 4145H and 4330V tool steels
- ✓Finish grinding to gauge after hardfacing
- ✓Deposit thickness, carbide grade and final OD recorded for every tool
Service 02
CNC Turning, Milling and Mill-Turn for Oilfield Components
We machine new components from bar and forgings, and re-machine repaired tools back to drawing, so a rebuilt tool moves from welding to machining under one job and one traveler.
Materials: 4140, 4145H, 4330V, 17-4 PH, 316 and duplex stainless, Inconel 625 and 718, Monel K-500, beryllium copper and non-magnetic drill collar alloys.
Machining Capabilities
- ✓Turning: CNC turning with live tooling for long, heavy tool bodies
- ✓Milling: 3-, 4- and 5-axis machining centers, chosen by part geometry
- ✓Mill-turn: complete parts in one setup
- ✓Deep boring: long bores in tool bodies and housings
- ✓Threading: connections cut and gauged to your drawing and specification
- ✓Tolerances: held to your drawing and verified at final inspection
- ✓Volumes: one-off prototypes, small batches and repeat production
Service 03
Weld Overlay and Dimensional Rebuild
Worn does not mean scrap. We restore lost material on blades, journals, seal areas and bores, then machine the surface back to size. For corrosion and wear service, we clad with the alloy your application calls for.
Processes and Alloys
- ✓TIG (GTAW): manual precision TIG for small features and exotic alloys; a dedicated TIG machine for butter layers and build-up
- ✓MIG (GMAW) and flux core (FCAW): high-deposition build-up on large worn areas
- ✓Stick (SMAW): heavy-section repair and field work
- ✓Brazing: carbide insert and tile attachment
- ✓Powder and cored wire: wear-resistant overlays
- ✓Cladding alloys: Inconel 625, stainless and cobalt-based alloys
Service 04
Stabilizer and Precision Grinding to Gauge
Hardfacing is only as good as the grind that follows it. An out-of-round or over-gauge stabilizer sticks in the hole; an under-gauge one stops doing its job on day one.
We grind hardfaced blades and cylindrical surfaces to the gauge diameter and blade profile on your drawing.
What We Grind
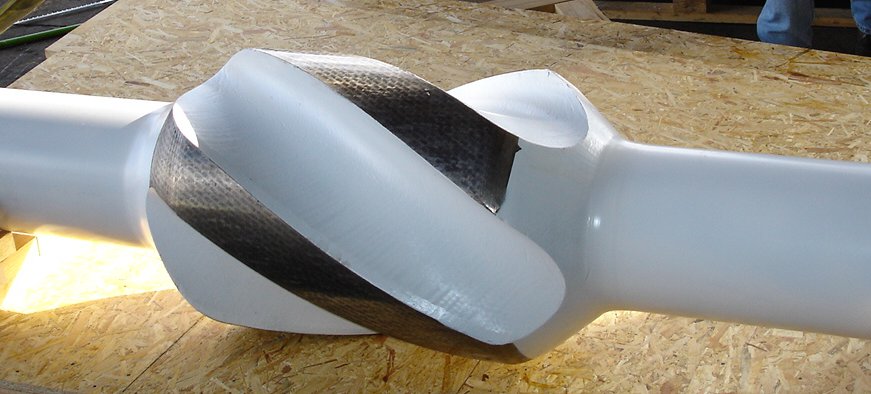
- ✓Spiral and straight blade stabilizers, sleeves, reamers and wear pads
- ✓OD and cylindrical grinding of shafts, mandrels and sleeves
- ✓CNC grinding from 8 to 24 in. diameter and manual grinding from 6 to 8.5 in. diameter
- ✓Gauge diameter ground to your drawing tolerance
- ✓Ring-gauge and dimensional report with each tool
Service 05
Sinker EDM for Internal Features
Some features cannot be reached with a cutter: internal keyways, blind slots, square-cornered pockets and shapes deep inside a hardened bore.
Sinker EDM burns them in with a shaped electrode, with no cutting force and no distortion.
EDM Capabilities
- ✓Internal keyways and splines in hardened or hardfaced parts
- ✓Several identical features sunk in one setup with multi-point electrodes
- ✓Deep reach inside long bores
- ✓Works on tool steel, Inconel, carbide and other hard-to-machine alloys
Service 06
Inspection, NDT and a Data Package With Every Tool
A repaired tool is only worth running if you can prove what was done to it.
Inspection and Records
- ✓Incoming inspection: dimensional check and wear map before any work starts, with a repair-or-scrap recommendation
- ✓Dimensional inspection: calibrated measuring instruments and product-specific profile gauges, with instrument IDs recorded on every report
- ✓Thread inspection: connection gauging to your specification
- ✓NDT: magnetic particle (MT), dye penetrant (PT) and ultrasonic (UT) by certified technicians
- ✓Hardness testing of base metal and overlay
- ✓Turnover package: material test reports, weld procedure and welder records, NDT reports, final dimensional report and serial-number traceability
What We Work On
Tools and Components We Work On
| Category | Typical items |
|---|---|
| Stabilization | Integral blade, sleeve-type and near-bit stabilizers; roller reamers |
| Hole opening and milling | Reamers, hole openers, junk mills, taper mills, section mills |
| Wellbore clean-up | Scrapers, brush tools, magnets, circulating subs |
| Drill string | Subs, crossovers, drill collars, kelly and saver subs |
| Motors and MWD | Bearing housings, rotor and stator housings, wear sleeves, kick pads |
| Fishing and intervention | Overshots, grapples, wash pipe shoes |
| Pumps and valves | Plungers, sleeves, seats, gate and ball trim |
How a Repair Job Runs
1. Quote — Send drawings or photos, or drop the tool off. We review it and send a quote.
2. Strip and inspect — Old hardfacing comes off; the tool is measured and crack-tested.
3. Report — You get a wear report and a firm price before repair work starts.
4. Rebuild and hardface — Worn areas are built up and the selected hardfacing is applied under controlled preheat.
5. Machine and grind — The tool is brought back to drawing dimensions and gauge.
6. Final inspection — Dimensional and NDT checks are recorded.
7. Ship — The tool leaves protected, tagged and with its data package.
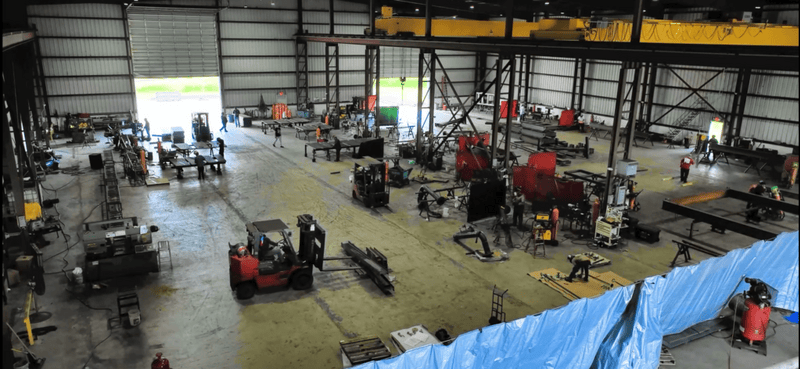
Inside Our Houston Fabrication Shop
Heavy Lifting Capacity — Two 15-ton overhead bridge cranes and two 1-ton jib cranes let us fit, flip, and load fully assembled skids without breaking the build into pieces.
25 Welders & Fitters — A full-time crew of AWS-certified welders and structural fitters runs your job in parallel, keeping multi-skid orders on one schedule.
Multi-Process Welding — MIG, flux-core, and TIG on carbon steel, stainless, and specialty alloys to AWS D1.1 and ASME B31.3 / Section IX procedures.
Structural & Piping Under One Roof — Skid bases, pipe spools, platforms, and supports are fabricated side by side, so fit-up problems are caught on our floor, not yours.
In-House Testing & QA — Hydrostatic testing, NDT, and Factory Acceptance Testing verify every unit before it ships.
Built for Heavy Haul — Minutes from 290 & Beltway 8 with crane-loaded, oversized-ready shipping and mobile crews for on-site setting and tie-ins. We have a storage yard as well!
Why Tool Companies Send Work to WeldIT
When a rig is waiting on a tool, you need one shop that owns the result from strip-down to final inspection.
Welding, machining, grinding and inspection run under one job, so nobody points at another vendor when a dimension is off.
We sit near US-290 and Beltway 8. Drop a tool off in the morning or let us collect it; no ocean freight, no customs, no two-week transit.
Two 15-ton overhead cranes and heavy-haul access handle full-length drilling tools.
25 welders and fitters qualified to ASME and AWS standards.
Material traceability, weld records and inspection reports ship with the tool.
Rush turnaround is available when a rig is waiting on a tool. Call us to check current capacity.
FAQs
Hardfacing, Machining & Downhole Tool Repair
Straight answers on hardfacing selection, repair, capacity and documentation.
Hardfacing is a layer of wear-resistant material, usually tungsten carbide in a metal matrix, welded or brazed onto the surfaces of a tool that rub against rock or steel. It protects the softer tool body and extends run life.
Crushed carbide composite is the economical choice for soft to medium formations. Carbide inserts suit medium formations. Carbide tile, in brick or herringbone patterns, lasts longest in hard, abrasive rock. Tell us the formation and footage target and we will recommend one.
Usually, yes. We strip the old hardfacing, check the body for cracks, rebuild the blades, re-hardface and grind back to gauge. If the body fails inspection, we tell you before you spend money on it.
We grind tools from 6 to 24 in. in diameter. Send us the length and weight of your tool and we will confirm fit before you ship it.
It depends on wear and the hardfacing system chosen. You get a firm date with the quote, and rush service is available when a rig is waiting.
Both. We machine new components from bar or forgings to your drawing, and we re-machine repaired tools.
Alloy tool steels such as 4140, 4145H and 4330V, stainless and duplex grades, nickel alloys such as Inconel and Monel, and non-magnetic drilling alloys.
A final dimensional report, NDT reports, weld records and material traceability, tied to the tool serial number.
Yes, across Greater Houston. We also receive tools by freight from outside the area.
TESTIMONIALS
What Our Clients RAVE About!
Posted on Google
 Claudine Jones234 days ago
Trustindex verifies that the original source of the review is Google.
Very professional. Nice work.Posted on Google Josh239 days agoWeld It, is an outstanding company there service and customer support is top-tier! we called them for an emergency weld repair on a mixer they responded quickly scheduled the next day and got the repair done in time. Great work Guys Thank you!+0Posted on Google
 david misra250 days agoWeldiT was very professional . They stayed in budget and finished on time. Excellent pricing and service. Highly recommend.Posted on Google
 Kam295 days agoWeldit exceeded our expectations from start to finish. Their team is extremely professional and highly knowledgeable in MIG aluminum welding. They took the time to understand the project, explained the process clearly, and delivered clean, precise welds with top-tier craftsmanship. What really stood out was their reliability they completed the project exactly within the timeframe they promised, with no delays and no surprises. The quality of work, attention to detail, and commitment to deadlines truly set Weldit apart. If you’re looking for a welding company you can trust for skill, professionalism, and on-time delivery, Weldit is the clear choice.+2Posted on Google
 Luis George Jr295 days agoAmazing quality and super accommodating for everything I requested regarding our pipeline project in Houston. Saul has a a crew who are super professional and experts at what they do ! Will definitely be using WeldiT for all our welding needs…Posted on Google
 Alex West296 days agoExcellent work! Very professional! We will definitely be back!!!Posted on Google
 Aymaan299 days agoWeldiT came and did all of our vacuums which were stainless steel and they came and conquered. Would highly recommend them for the work they’ve done, especially with stainless steel or aluminum. They make a promise and they live up to their promise and the work is done on the highest quality. Thanks WeldiT we’ll definitely be using them for our next car wash project.+3Posted on Google
 Roy Roy306 days agoAmazing company! We had them repair our gate and metal fence. Their welders and helpers did a great job fabricating and installing our steel fence. Highly recommended!Posted on Google
 Emrose Rodrigues306 days agoBest company n trustworthy for welding servicesVerified by TrustindexTrustindex verified badge is the Universal Symbol of Trust. Only the greatest companies can get the verified badge who has a review score above 4.5, based on customer reviews over the past 12 months. Read more


Get Your Tools Back in the Hole Faster
Send us a drawing, a photo of the wear, or the tool itself. We will tell you what it needs, what it costs and when you will have it back.